China Top Golf Ball Manufacturers 10M+ Balls Monthly
China’s golf-ball industry combines large-scale production with specialized molding, curing, and finishing operations. This introduction examines manufacturers associated with Monthly Capacity 10M+ Balls, a figure that signals substantial output—but does not, by itself, prove consistent quality or dependable delivery. Buyers should look beyond headline numbers.
Golf-ball designer Dean Snell has said, “The golf ball is the only piece of equipment you use on every shot.” That principle makes production control especially important. A small change in core compression, cover thickness, or paint application can affect feel and flight. Ask manufacturers how they test these variables, track production batches, and handle samples before approving a full order. Concrete records matter. So do repeatable results.
A factory producing millions of balls each month may serve several markets and product tiers. Its available capacity for a particular design could be lower. That distinction is easy to miss. Request details on ball construction, testing methods, lead times, and quality checks, then compare them with independent sample testing where practical. Capacity claims deserve verification. So do certification documents and stated defect rates. Even careful sourcing has limits: one successful sample cannot guarantee every shipment will perform identically. The following overview considers manufacturers through that practical lens, weighing production scale alongside evidence of process control, communication, and product consistency.
China’s Golf Ball Industry: Manufacturers with 10M+ Balls in Monthly Capacity
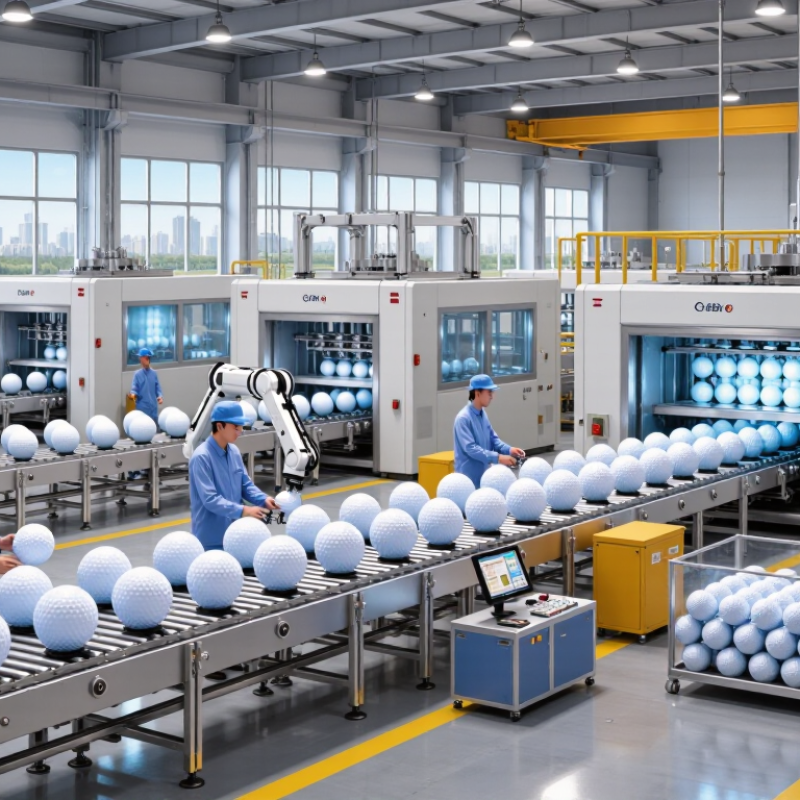
China’s golf ball industry includes manufacturers that report monthly capacities above 10 million balls. This scale usually depends on coordinated production lines, steady material supply, and disciplined quality checks. Capacity alone, however, does not show how many finished balls a factory can ship each month. Buyers should distinguish rated output from recent, verified production.
A useful assessment looks beyond a headline figure. Ask for monthly production records, sample lead times, and the factory’s process for checking ball weight, diameter, compression, and surface finish. On the production floor, consistent molding and evenly applied coatings matter; small differences can affect feel and flight. Also check whether packaging and inspection can keep pace with molding. It is easy to overlook this bottleneck.
Tips: Request a dated capacity statement and compare it with recent shipment records. Ask how the factory handles peak orders and rejected batches. If possible, inspect samples from different production runs, not just one polished set. Numbers are helpful, but they need context. A little uncertainty is normal.
USGA/R&A Ball Limits: At Least 42.67 mm Diameter and No More Than 45.93 g
At a monthly output of 10 million golf balls, small dimensional variations can become a serious quality issue. USGA and R&A equipment rules require a conforming ball to measure at least 42.67 mm in diameter and weigh no more than 45.93 g. The limits work in opposite directions: diameter has a minimum, while mass has a maximum. Simple, but easy to misread. A ball may be larger than the minimum diameter, but it cannot exceed the weight cap. Reliable production checks use calibrated gauges and precision scales, rather than visual inspection alone. Measurements across shifts and batches can reveal changes caused by mold wear, material variation, or process temperature.
Meeting these two limits does not, by itself, establish full conformity; other performance requirements and formal evaluation may also apply. I would not treat one perfect sample as proof of a consistent production run. Batch records and repeat measurements give buyers a clearer picture of process control. A useful check is to compare readings from different points in a run, not just the first balls off the line. Small differences matter. Measurement tools also need regular calibration, or precise-looking numbers may be misleading.
Golf Ball Structure: Core, Cover, and Dimple Design Across Product Types
A golf ball’s performance comes from three parts working together: the core, cover, and dimple pattern. The core stores and releases energy at impact. Firmer cores can support faster ball speed, while softer constructions may feel more responsive on short shots. The cover shapes durability, spin, and feel. Surlyn-style ionomer covers are generally durable; urethane covers can offer more greenside spin, but may scuff sooner. No single choice suits every player.
Dimple design manages airflow around the ball. Dimples help reduce drag and create lift, influencing trajectory and distance. Their depth, shape, and arrangement matter, though the result depends on the full construction—not one feature alone. Two-piece balls often prioritize durability and distance for recreational play. Multi-layer designs can separate driver performance from approach-shot control. That sounds neat, but real results vary with swing speed, weather, and contact quality. Manufacturers assess prototypes through compression checks, launch measurements, and repeated impact testing. A ball that feels soft in a warm factory may behave differently on a cold course. Small details count. Even then, choosing the right balance can take a few rounds.
Golf Ball Structure by Product Type
Typical layer architecture across common golf ball constructions
Two-piece balls typically combine a core and cover. Three-piece and multilayer designs add one or more mantle layers between them. Dimples shape the ball’s aerodynamic surface; their pattern and count vary by design and are not represented as structural layers here. Actual constructions vary by model.
Factory Quality Control: Testing Compression, Weight, Diameter, and Flight
At a factory producing millions of golf balls each month, quality control depends on repeatable checks, not visual judgment alone. Samples from each production run are measured for weight and diameter using calibrated scales and gauges. Small differences matter. A ball that falls outside the agreed range may behave differently, even when its surface looks flawless.
Compression testing helps assess how much a ball deforms under a fixed load. Technicians record results and compare them with the product specification, while checking that testing equipment stays properly calibrated. Flight tests add another layer: balls are struck under controlled conditions, then their launch, direction, and distance are observed. Temperature and launch setup can affect results, so records need to include the test conditions. This process is useful, but not perfect. Gauges can drift, and busy shifts may leave gaps in documentation. Reviewing unusual readings and repeating questionable tests helps catch problems before a batch moves forward. Quality checks work best when measurements are traceable and teams are willing to question results that seem too neat.
China Top Golf Ball Manufacturers 10M+ Balls Monthly - Factory Quality Control: Testing Compression, Weight, Diameter, and Flight
The sample readings below are illustrative process-control data, not results attributed to a specific factory or brand. Golf-ball conformity requirements are distinguished from optional internal production targets.
| Quality Check | Measurement | Reference or Control Criteria | Illustrative Sample Result | Typical Inspection Method |
|---|---|---|---|---|
| Compression | Relative deformation under a specified load; often reported as a compression rating | No single universal golf-ball compression rating is required by the Rules of Golf. Set a product-specific target and test method. | Target 90; sample readings 88–92 (illustrative) | Calibrated compression tester; condition samples consistently for temperature before testing. |
| Weight | Mass per ball | Rules of Golf limit: no more than 1.620 oz (45.93 g). | 45.4–45.7 g (illustrative; below the maximum) | Calibrated precision balance; record individual readings and lot variation. |
| Diameter | Outside diameter at multiple orientations | Rules of Golf minimum: 1.680 in (42.67 mm). There is no corresponding maximum diameter in this minimum-size requirement. | 42.70–42.76 mm (illustrative; above the minimum) | Calibrated diameter gauge or optical measuring system; check several axes. |
| Roundness and symmetry | Dimensional variation and performance consistency when oriented differently | Golf-ball conformity includes symmetry requirements; a ball must not be designed, manufactured, or intentionally modified to have properties that differ from those of a spherically symmetrical ball. | Within the plant’s documented dimensional and orientation-variation limits (illustrative) | Multi-axis dimensional checks and, where required, testing under the applicable official conformity procedure. |
| Flight and distance | Carry, total distance, launch, spin, and directional consistency | Use the applicable governing-body test protocol for conformity; internal flight targets should be defined for the specific ball model and test setup. | No out-of-limit readings in the illustrative sample; results depend on the test conditions and are not a conformity certification. | Launch monitor or controlled robot test; standardize club, speed, launch conditions, balls, and environmental settings. |
| Lot sampling and traceability | Sample identification, inspection frequency, and recorded results | Define a documented sampling plan and acceptance criteria for each production lot; retain calibration and inspection records. | Illustrative example: 32 balls sampled per lot, with results logged by batch and test date. | Use a written inspection plan, calibrated equipment, and traceable records; sample size should be set by the manufacturer’s quality system. |
Supplier Evaluation: Comparing Production Capacity, Standards Compliance, and Exports
A supplier claiming monthly output above 10 million golf balls should be assessed by more than its headline figure. Ask how much capacity is currently available, not just installed. Review recent production records, shift schedules, and examples of peak-season planning. A factory tour can help, but it cannot replace consistent batch data. Numbers can mislead.
Standards compliance also needs practical verification. Request current certificates, test methods, and sample inspection records for core measures such as weight, diameter, compression, and paint durability. Confirm that the documents cover the specific product and production site. Then compare export experience with your target market: ask about shipment history, packaging specifications, lead times, and document accuracy. A smooth first shipment matters; repeatability matters more. One detail is easy to overlook: a capable factory may still need time to adapt its packaging or inspection process.
Tips: Ask for a recent, anonymized batch report and match it against a physical sample. Clarify how rejected units are recorded and corrected. If answers are vague, pause and request written evidence. No checklist catches everything, and even strong suppliers can have occasional inconsistencies. Judge how openly they explain them.